Overview
This 100 TPD sodium hypochlorite plant is a full engineered EPC-grade continuous production system built for mega-scale municipal and heavy industrial projects. Its rated design point is 100 tons of 12% sodium hypochlorite liquid daily, with adjustable output concentration across 5% to 15% NaClO. It uses mature ion-exchange membrane brine electrolysis technology and runs on industrial salt, softened feed water and grid power only.
When chlorine demand hits this scale, relying on bulk delivered bleach becomes a major supply chain bottleneck. Hazardous chemical transport permits, truck scheduling, storage tank rotation and natural chlorine decay in storage all add up to unpredictable operational risk. On-site generation removes these variables. You produce fresh hypochlorite continuously, dial in the exact strength your process requires, and cut long-term chemical logistics spend.
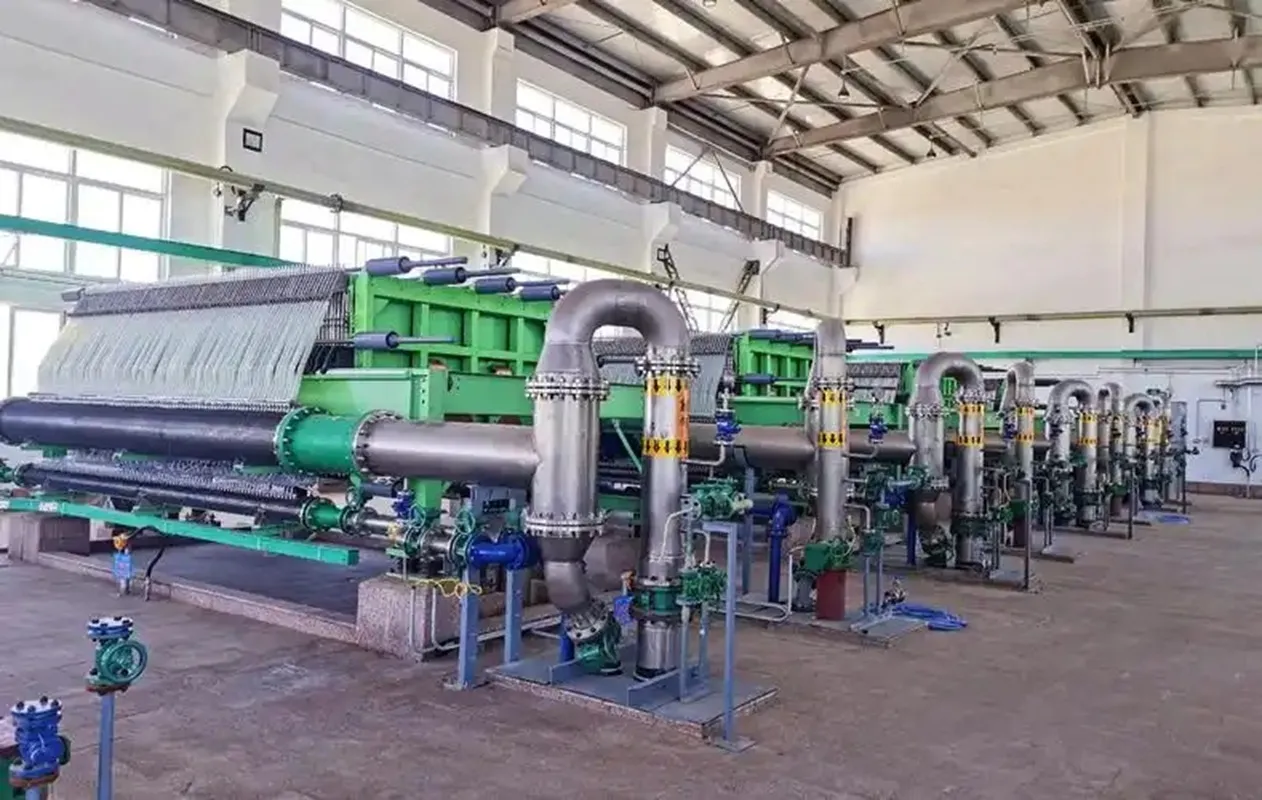
This is not a simple multi-skid assembly. It is a complete process package: brine softening & preparation station, parallel electrolyser banks, high-power rectifier house, closed cooling water circuit, hydrogen vent & dilution safety system, finished product buffer tank farm, central DCS control room and full safety interlock network. Built for non-stop 24/7 year-round operation. Modular phased construction is supported, so clients can start with part capacity and expand electrolyser stacks later.
Typical end users include large city water & wastewater authorities, integrated pulp and paper mills, major oilfield produced water hubs, large mining complexes and regional industrial park central disinfection stations.
Core Specs
| Specification | Detail |
|---|---|
| Rated daily output | 100 ton/day sodium hypochlorite liquid @ 12% concentration |
| Adjustable concentration range | 5% ~ 15% NaClO |
| Fixed daily available chlorine | 12,000 kg/day |
| Core technology | Ion-exchange membrane brine electrolysis |
| Raw materials | Industrial salt (NaCl ≥89%), softened fresh water, electricity |
| Standard consumption | ~2 kg salt, ~2.5 kWh DC power per kg available chlorine |
| Control system | Redundant PLC + DCS, SCADA native integration, full safety interlock, historical data logging & remote access |
| Wetted materials | CPVC piping, 316L stainless steel, fluorine rubber gaskets, titanium coated electrode |
| Layout | Multi-block EPC process plant; phased modular build option |
| Floor space | 600 ㎡ |
| Unit total weight | 52 ton |
| Warranty | 12 months full package; extended maintenance contract for ion membrane stacks & electrode banks |
| Field support | Full set civil, electrical, piping & P&ID drawings, site construction supervision, commissioning, shift crew training, 24/7 remote troubleshooting, regional service in Africa, Middle East & Southeast Asia |
Output Table by Concentration (Fixed 12,000 kg/day available chlorine)
| NaClO Concentration | Daily Liquid Output |
|---|---|
| 5% | 240.0 TPD |
| 8% | 150.0 TPD |
| 10% | 120.0 TPD |
| 12% | 100.0 TPD (rated) |
| 15% | 80.0 TPD |
Important note: Total available chlorine capacity remains unchanged. Lower concentration settings deliver larger liquid volume; higher concentration reduces liquid throughput accordingly.
OPEX Breakdown (Reference, running at rated 12% mode, 24h continuous)
Calculated based on 12,000 kg available chlorine per day
- Salt consumption: ~24,000 kg/day industrial salt
- DC power consumption: ~30,000 kWh/day
- Water consumption: ~80 m³/day (brine softening, process & cooling make-up water)
- Consumable cycle: Ion membrane replacement every 2–3 years; electrode overhaul / re-coating every 3–5 years
- Labour: 3-shift operation team, supervisor + dedicated full-time maintenance engineer; auto unattended run under stable conditions
Actual operating cost depends heavily on local electricity tariff, bulk salt contract price, water treatment cost and raw water hardness. We provide custom OPEX and TCO evaluation once you share local utility rates and water quality report.
Key Benefits
- Full concentration flexibility. One integrated plant covers low-concentration municipal water disinfection and high-strength bleaching feed, eliminating the need to source different bleach grades.
- Stable fresh chlorine supply. Sodium hypochlorite degrades steadily during storage; continuous on-site generation guarantees consistent available chlorine for critical processes.
- Tiered redundant safety design. Continuous hydrogen monitoring with multi-stage alarm & shutdown logic, brine low-level interlock, over-temperature protection, pressure relief, dedicated explosion-proof vent stack and containment bunding, mandatory for this scale of electrolysis facility.
- Seamless DCS / SCADA integration. Supports Modbus and mainstream industrial communication protocols, ready to connect with site-wide central control systems for large EPC projects.
- Phased expandable architecture. If future chlorine demand rises, additional electrolyser modules can be retrofitted without rebuilding the whole civil foundation and utility network.
Typical Applications
- Mega municipal drinking water & wastewater disinfection complexes
- Pulp mill and large integrated textile bleaching production lines
- Oilfield & mining produced water and injection water treatment
- Industrial park circulating cooling water biocide control
- Large-scale seafood & aquaculture zone central sanitation
- Central chemical supply station for heavy industrial clusters
FAQ
Q: Can I switch between different concentrations while running continuously? A: Yes. Adjust brine feed and dilution setpoints on the DCS console. Allow 90–120 minutes for the whole electrolyser bank, cooling loop and buffer system to stabilise before sampling and verifying finished concentration.
Q: What site infrastructure is mandatory for the 100TPD plant compared with smaller 1/5/10/30/50TPD models? A: It requires dedicated high-capacity power transformer station, full raw water softening pretreatment package, independent hydrogen vent & dilution stack, hazardous chemical containment bund, explosion-proof electrical zoning, fire protection system and large on-site product tank farm. We deliver complete civil, electrical and utility requirement drawings after order confirmation.
Q: What voltage and frequency versions are available? A: Standard 380V 50Hz; 415V, 440V, 480V / 60Hz custom options. Rectifier cabinets are fully matched to your local grid specification.
Q: How long will commissioning take for this EPC-scale package? A: 14–21 working days on site, provided civil foundation, power supply, water supply and drainage are completed and accepted. Our engineers carry out full safety interlock testing, process tuning and three-shift operation & maintenance training for your permanent crew.